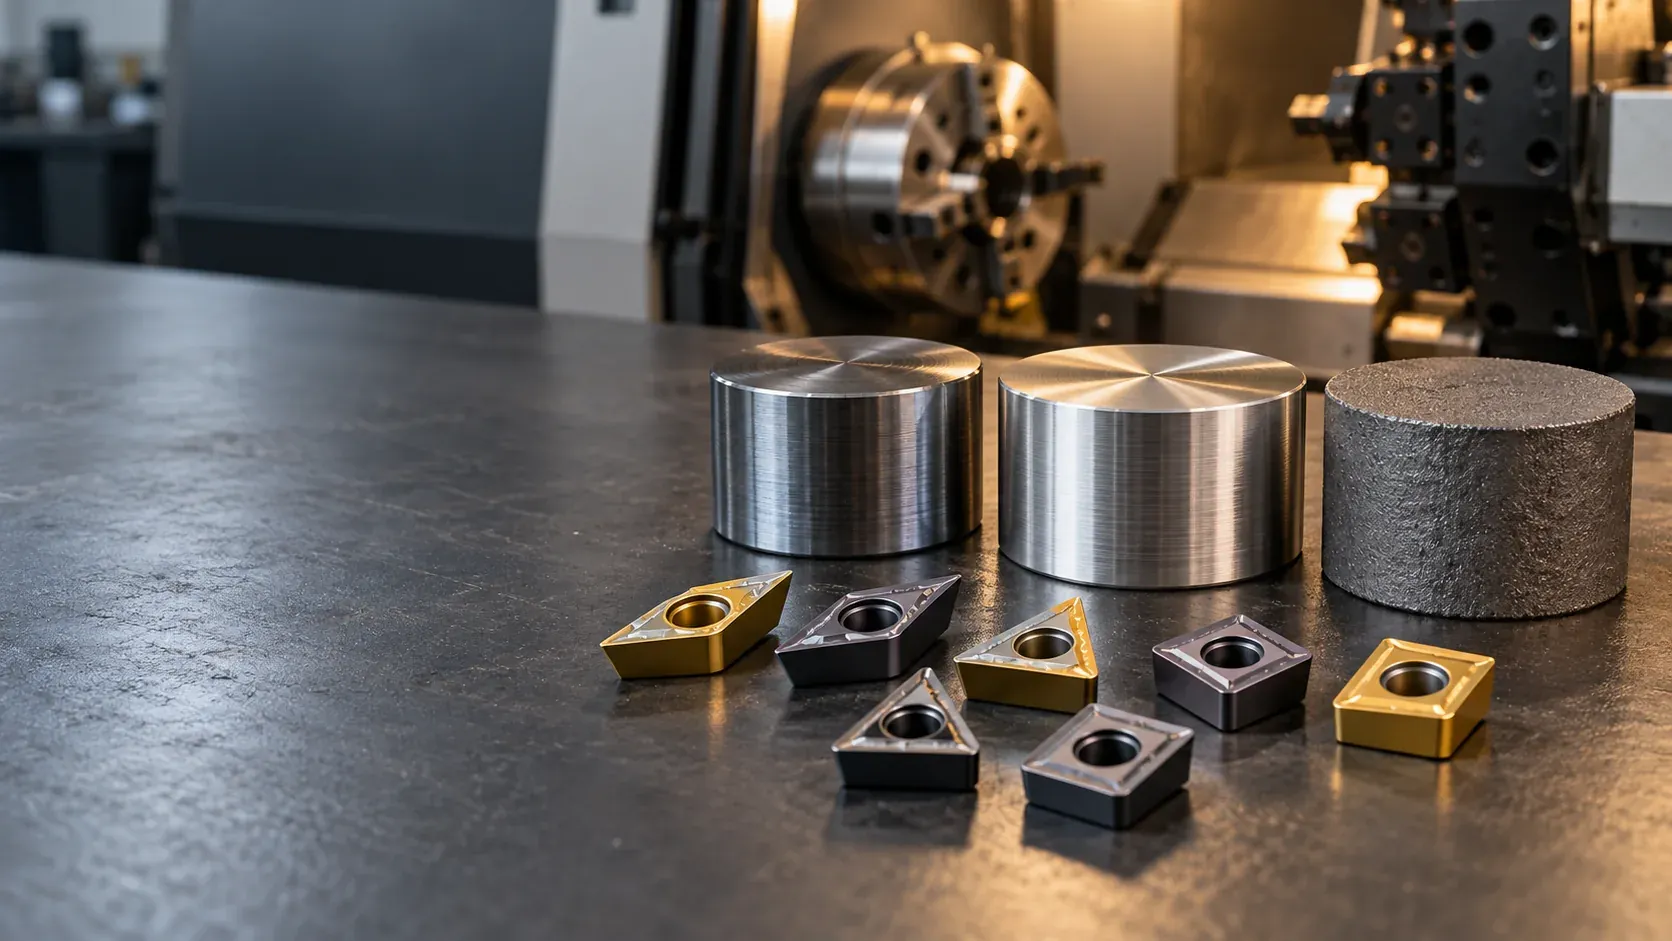
Carbide Insert Grades for Steel, Stainless Steel and Cast Iron
Choose a turning insert starting point by material, cut and current tool code.
Read the guide →CNMG, WNMG, TNMG, DNMG, CCMT, SNMG and VNMG inserts for steel, stainless steel, cast iron and aluminum.
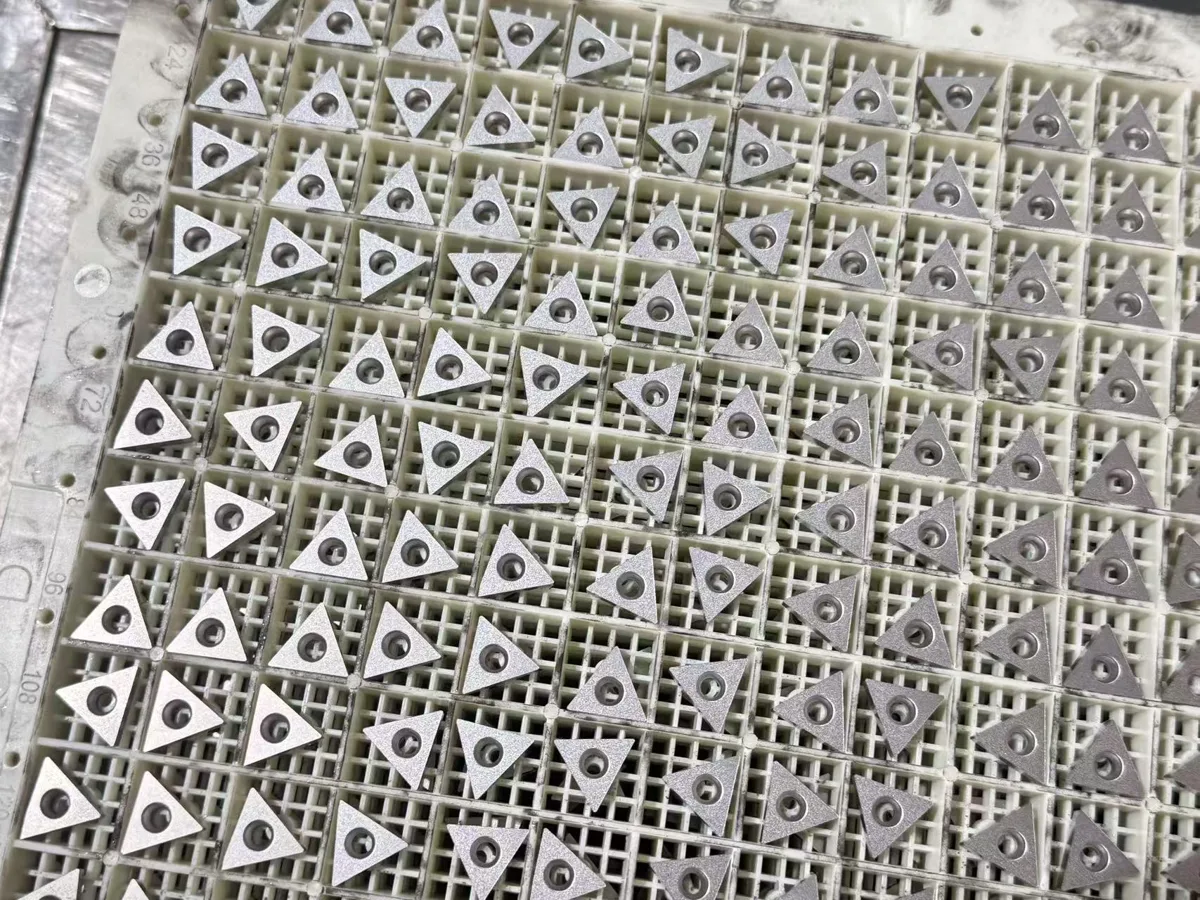
CNMG120408, WNMG080408, TNMG160408, DNMG150608, CCMT09T308, SNMG120408
ISO code, workpiece material, holder model, operation, failure mode and quantity.
For standard replacement parts, send the model code and quantity. For OEM parts, send a drawing, sample photo or model list. Our team checks shape, grade, coating, tolerance and packing before offering.
ISO code, model list, drawing or sample photo.
Material, operation, machine and current cutting problem.
Coating, substrate and geometry are matched to the job.
MOQ, delivery, OEM packing and batch inspection are confirmed.
Know the job but not the code? Start from the material you cut. Each group below names the problem that group causes, the models buyers usually check first, and the guide section that explains the choice.
General steels and alloy steels. The starting point for most external turning: a medium chipbreaker on an 80° insert covers roughing to semi-finishing. Buyers usually check CNMG120408 or WNMG080408 first, and SNMG120408 for heavy roughing.
Stainless sticks, work-hardens and builds up on the edge. A sharper chipbreaker class and steady chip control matter more than a harder edge. Positive inserts such as CCMT09T308 are common on smaller lathes and boring work.
Short chips, abrasive wear and often an interrupted surface. Toughness and edge support come first: CNMG120408 and SNMG120408 are the usual starting points, confirmed against your surface condition.
Working on aluminium, heat-resistant alloys or hardened steel instead? See all six material groups (P, M, K, N, S, H). Choosing between the two 80° workhorses? Read the CNMG vs WNMG comparison before you change holder systems.
These are the turning models we cover as standard. Find yours, check the typical chipbreaker class and material groups, then send the full code — or your whole list — through the single inquiry entry on this page. For the most-ordered size, see the CNMG120408 family page — dimensions, chipbreaker classes and 10-piece trial supply. Availability and the proposed specification are confirmed in your quote.
| Model | ANSI | Typical chipbreaker class (starting point) | Stainless version | Material groups |
|---|---|---|---|---|
| CNMG120408 | CNMG432 | Medium | Sharp (MS class) | P · M · K |
| WNMG080408 | WNMG432 | Medium | Sharp (MS class) | P · M · K |
| CNMG120404 | CNMG431 | Finishing–medium | Sharp (MS class) | P · M |
| TNMG160408 | TNMG332 | Medium | Sharp (MS class) | P · M |
| VNMG160408 | VNMG332 | Finishing (profiling) | Sharp (MS class) | P · M |
| DNMG150608 | DNMG442 | Medium | Sharp (MS class) | P · M |
| SNMG120408 | SNMG432 | Roughing | — | P · K |
| WNMG080404 | WNMG431 | Finishing–medium | Sharp (MS class) | P · M |
| CCMT09T308 | CCMT32.52 | General purpose (positive) | Same insert family | P · M |
| CCMT09T304 | CCMT32.51 | General purpose (positive) | Same insert family | P · M |
| CCMT060204 | CCMT21.51 | General purpose (positive) | Same insert family | P · M |
| DCMT11T308 | DCMT32.52 | Finishing (profiling, positive) | Same insert family | P · M |
Chipbreaker classes shown are the standard configuration for each model; exact suffix and grade are confirmed in your quotation, in writing. Full size data: insert size chart.
Your code is not listed? Send the complete label or a clear photo. These examples are a starting point for matching. And if the code on your insert has worn off completely, use our free photo identification service.
Use these details to compare a suitable option. Grade availability and cutting recommendations are confirmed for your application.
| Selection step | What to check |
|---|---|
| Fit and geometry | Full ISO code, holder model, insert size and corner radius |
| Material and operation | Steel, stainless steel, cast iron or aluminum; roughing or finishing |
| Grade and chip control | Current grade, chipbreaker, coating and edge-failure photo |
| Trial and repeat supply | Quantity per model, destination and packing preference |
A model or shape match alone does not establish equivalent cutting performance. Confirm the tool fit and evaluate the proposed grade before a repeat order.
Choose a turning insert starting point by material, cut and current tool code.
Read the guide →We will check the proposed model, grade, quantity and packing with you before confirming a quote.
10 pieces per model — one standard box. Models cannot be mixed to reach the minimum. Full ordering terms are on the supply range page.
Yes. A trial starts from 10 pieces of one model, so you can score it on your own machine and material before committing. Sample and trial quantities typically take 7–15 days; the confirmed date is in your quotation.
Yes — neutral packing is available at standard quantities, and private label packing starts from 2,000 pieces per model.
Stainless is group M. Start from the stainless section of the material groups guide, then confirm the chipbreaker class against your operation — stainless usually needs the sharper version of the same model.
Yes. Send clear photos through the photo identification service and we will identify the most likely ISO code with you before quoting.
Send the complete codes and quantities you have. Add the material, holder or cutter details when available so we can check the right supply options.
Paste your list into the inquiry. Attach drawings or photos in WhatsApp or email. Stocking for resale? See distributor supply terms.