APKT vs APMT Inserts: The Tolerance-Class Difference & Are They Interchangeable?
APKT and APMT are often searched together, but replacement decisions should start with cutter compatibility, not a similar-looking insert photo.
Quick difference
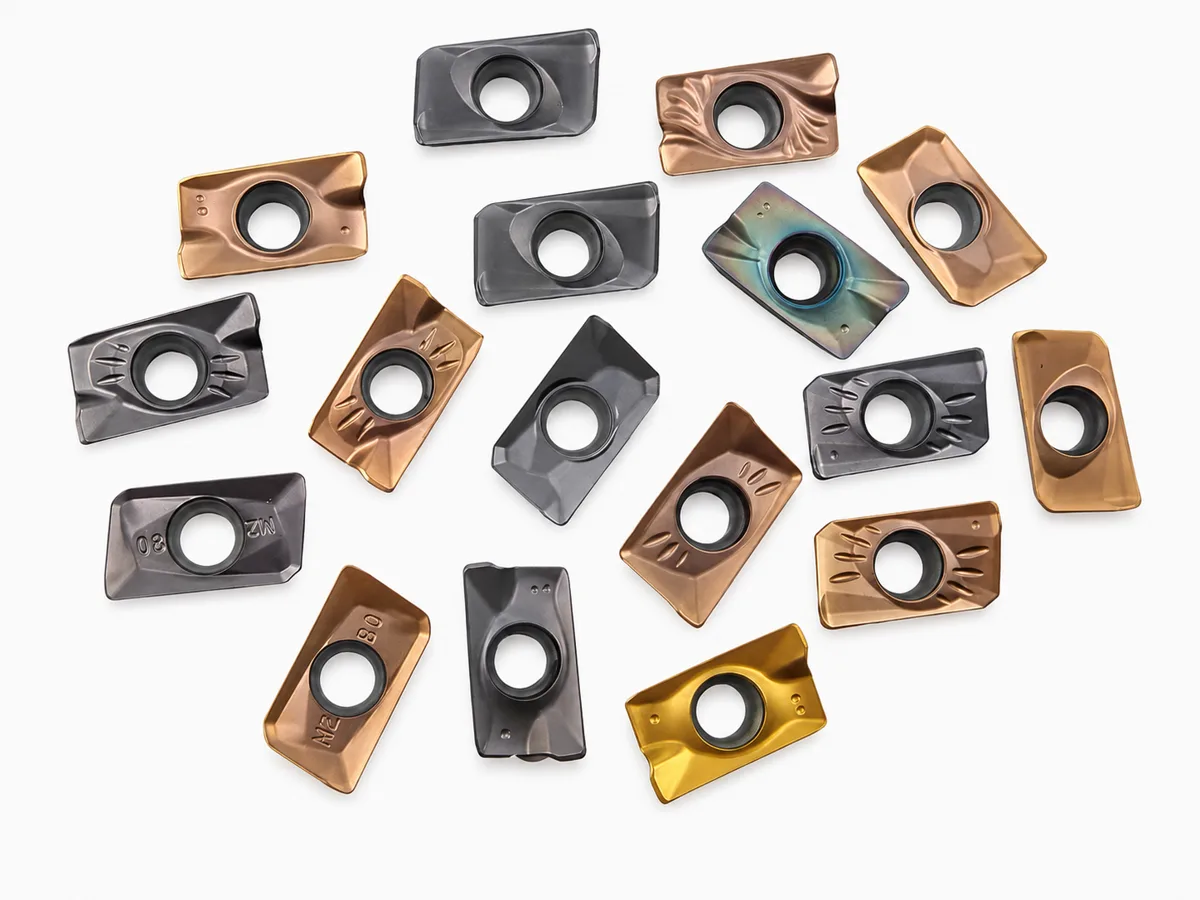
APKT and APMT share the same basic shape (A), 11° relief angle (P) and hole/chip-form code (T). The main designation difference is the third letter: K or M = tolerance class. K class controls nose height and thickness more tightly than M class. Tolerance class does not tell you the right grade, coating or application — and it does not guarantee an APKT insert fits an APMT cutter pocket.
| Feature | APKT | APMT |
|---|---|---|
| Basic shape | A parallelogram | A parallelogram |
| Relief angle | P 11° | P 11° |
| Tolerance class | K | M |
| Nose-height / edge-position tolerance (m) | ±0.013 mm | ±0.08–0.20 mm (size-dependent) |
| Thickness tolerance (s) | ±0.025 mm | ±0.13 mm |
| Automatically interchangeable | No | No |
Tolerance values are ISO 1832 tolerance-class values and vary by insert size; confirm the datasheet for a specific model before ordering. These are class-level references, not a dimensional guarantee for an individual APKT or APMT model. ISO 1832:2017 reference (Tables 1–3).
Do not choose APKT or APMT only by the family name. Confirm the full insert code, cutter body model, insert seat, screw or clamp arrangement, workpiece material and operation. Those details decide whether a replacement can be fitted and used safely.
Why this comparison matters
Buyers often search “APKT vs APMT” after receiving a model list, finding a used cutter body, or trying to replace inserts from another supplier. The names are close, and the inserts can appear similar at a glance. That is not enough for a purchasing decision. Insert designation, size, thickness, corner geometry, edge preparation and mounting arrangement can all change the real compatibility.
The most useful question is not “which family is better?” It is “which insert is specified for this cutter body and operation?” A correct answer needs the cutter information as well as the insert code.
Step 1: Read the complete code instead of only APKT or APMT
The family prefix is only the beginning. An RFQ should include every character visible on the box or insert label. If a code is incomplete, send clear photos of the insert from the top, side and seating surface. A supplier can then compare the geometry and identify which dimensions still require confirmation.
- Record the full insert code and any grade or coating marking.
- Check whether the insert has a single-sided or double-sided seating arrangement.
- Note the corner radius, thickness and visible chipbreaker.
- Do not mix a family name with an assumed size when the original code is unavailable.
Step 2: Confirm the cutter body, insert seat and screw
The cutter body is the controlling part of the assembly. It determines where the insert sits, how it is clamped and how the cutting edge is positioned. An insert that is close in shape can still be wrong for the pocket, screw angle or support surface. Fitting an unconfirmed insert may cause poor seating, vibration or damage to the cutter body.
| What to check | Why it matters | Useful RFQ evidence |
|---|---|---|
| Cutter body model | Confirms the intended insert family and mounting direction. | Model marking or a clear cutter photo. |
| Insert seat | Shows contact surfaces and support geometry. | Photo with the insert removed and seat cleaned. |
| Screw or clamp | Controls fit and clamping force. | Photo of the screw head and insert hole. |
| Existing insert | Allows comparison of code, size and chipbreaker. | Top, side and bottom photos. |
Step 3: Match the insert direction to the milling operation
After compatibility is confirmed, select the grade, coating and edge direction around the real operation. Shoulder milling, face milling, slotting and intermittent cuts load an insert differently. The workpiece material, machine rigidity, cutter overhang, coolant and required finish should be part of the discussion.
For example, a buyer machining a stable steel shoulder may prioritize predictable chip control and surface finish. A buyer dealing with interrupted cuts, casting skin or less rigid workholding may need to focus first on edge support and stability. These are process questions; the insert family alone does not provide the answer.
Step 4: Use one controlled trial before a repeat order
When an exact replacement is uncertain, a small controlled trial is more useful than changing insert family, grade and cutting conditions at the same time. Keep the cutter body and workpiece stable, confirm seating, then inspect the edge and chip after the test. This produces usable feedback for the next order.
Illustrative application example
Suppose a buyer needs replacement inserts for a shoulder-milling cutter but only has an incomplete APKT label. A useful first request would include the cutter body marking, a photo of the empty insert seat and the screw.
Those details help check the cutter pocket and mounting arrangement. Add the workpiece material and whether the job is roughing or finishing so the supplier can discuss a compatible option before an order is placed.
What to send for APKT or APMT matching
- Full insert code, if readable.
- Cutter body model and a photo of the insert seat.
- Top, side and bottom photos of the current insert.
- Workpiece material and operation: face milling, shoulder milling, slotting or finishing.
- Current issue, if any: chipping, vibration, poor finish or chip control.
- Required quantity, neutral packing or private-label requirement.
FAQ
Can I replace an APMT insert with APKT?
Start with the tolerance class in the code — K in APKT, M in APMT — then confirm the cutter body, insert seat and clamping arrangement. Only after the cutter body, insert seat and clamping arrangement are confirmed can the replacement be judged — it is determined by the specified cutter system, not by the family prefix alone.
Do I need to send cutting parameters before asking for a quote?
They are useful when you need grade or geometry support. If you do not have them, send the workpiece material, operation and current problem first.
Can you match a model from photos?
Photos can help identify the direction, especially when the full code is missing. A photo of the cutter body and insert seat makes the match more reliable.
Summary
APKT vs APMT is primarily a compatibility and application question. Start with the full code and cutter body, then confirm the seat and clamping arrangement, and finally choose the grade or geometry around the real operation. For related milling families, see our milling inserts product page and APKT/APMT milling insert guide. When ready, send your cutter body model, insert photos and quantity through the RFQ page.